
Lesson 6 - Hop Products
Isomerised Hop Pellets
Approximately 20% of the hops grown each year are used to produce isomerised products – and around 13% of these are isomerised hop pellets.
In order to isomerise the hop pellets, magnesium oxide is used as a catalyst. The magnesium oxide is added to the milled hops at a rate of 0.2 times the α-acids weight. The rest of the pelletisation process is similar to that used for T90s.
The packaged pellets are heat treated at a maximum temperature of 50°C and held there for 8-14 days. This results in about 99% of the α-acids being isomerised. This gives us a whopping hop utilisation of around 65%!
The finished iso-pellet has similar properties to a standard T90 pellet, but with iso-α-acids instead of α-acids and inferior aroma quality. The pellets break down quickly, so can be added to the kettle, or even the whirlpool, at any time.
An advantage is that they can be added late in the boil, or whirlpool, and achieve the bitterness target whilst also adding some late hop character. However, this advantage is reduced by the fact that less hops are now required as the utilisation is improved, thus less essential oil is added. Plus, the quality of the aroma is diminished by being heated for days.
Time to update the hop product overview diagram:
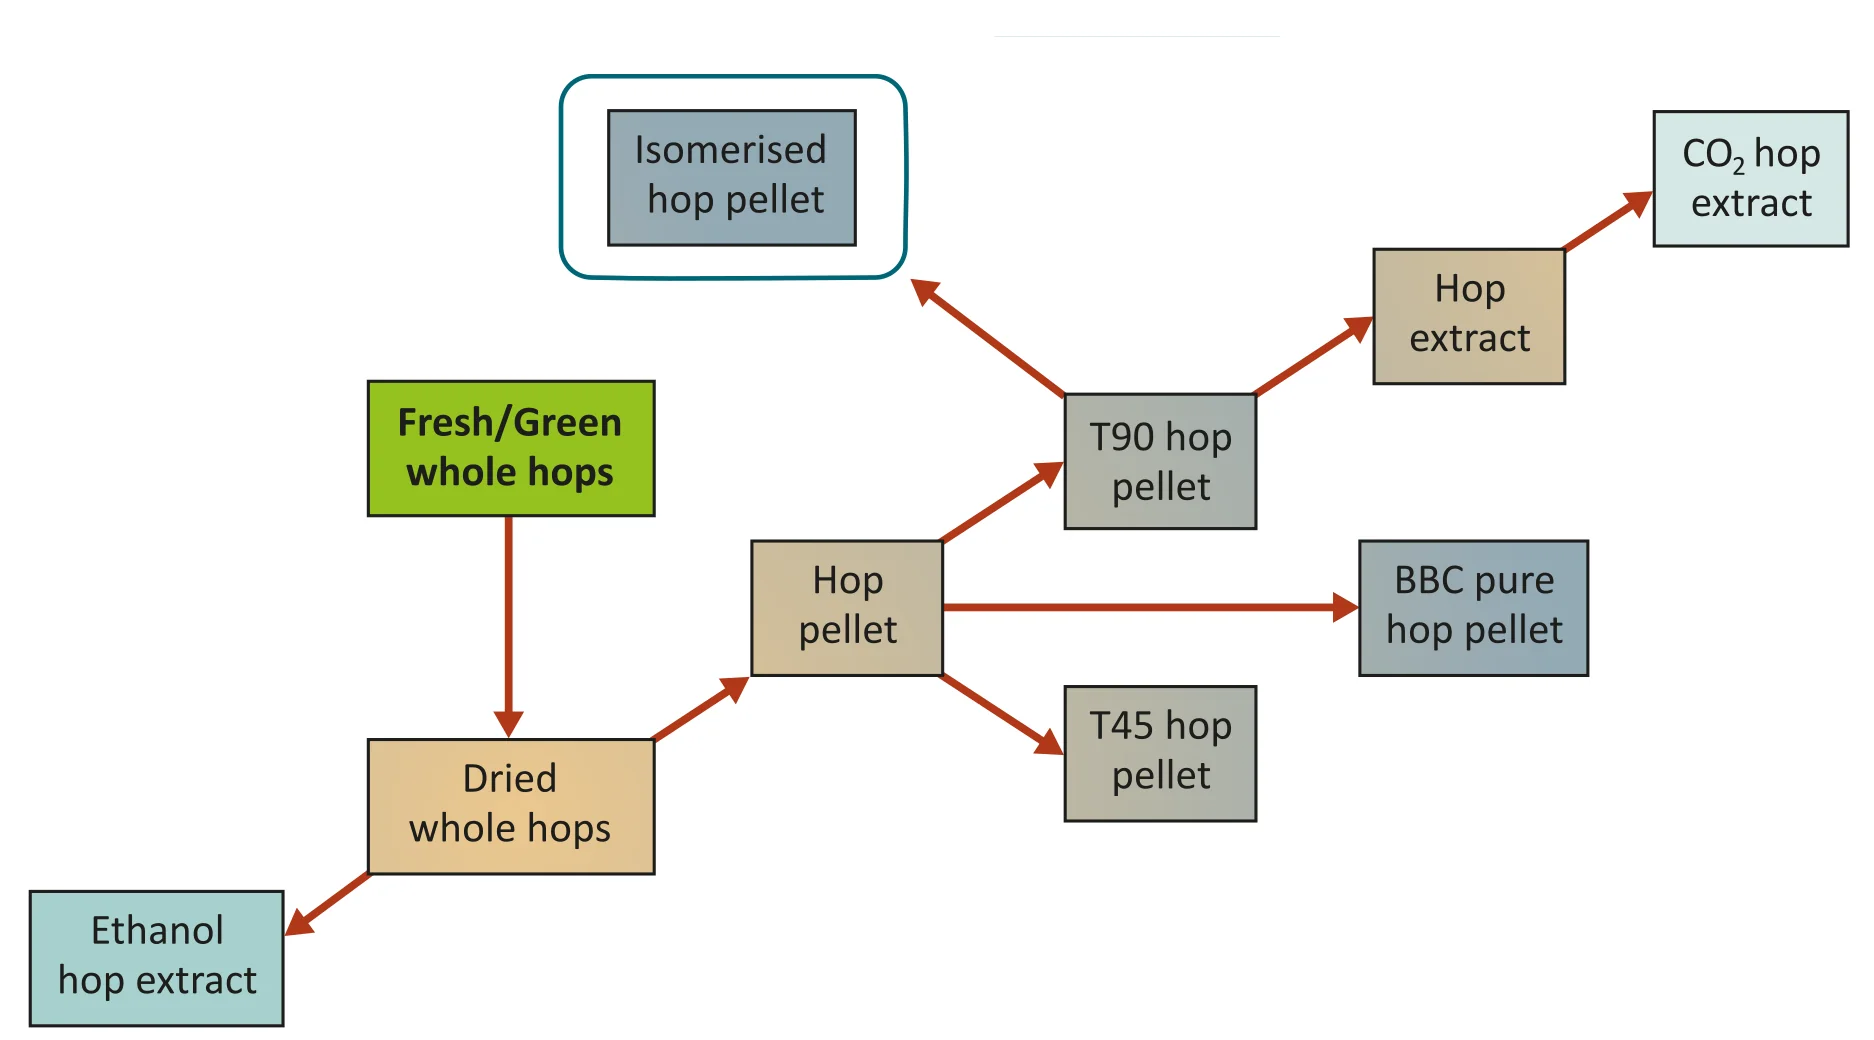
Figure: Overview of hop products and how they are typically derived
Can we do the same with hop extracts? Of course we can, and more!