
Lesson 6 - Malt Quality
This lesson deals with malt quality. We explore each parameter on a malt specification sheet and identify why they are specified. We then examine how they affect beer and the brewing process.
Malt Quality Parameters
We can divide malt quality parameters into groups.
The figure below shows the different categories, and parameters in each category. We consider each of these, looking at what the parameter is, why it is important, and how the analysis is performed.
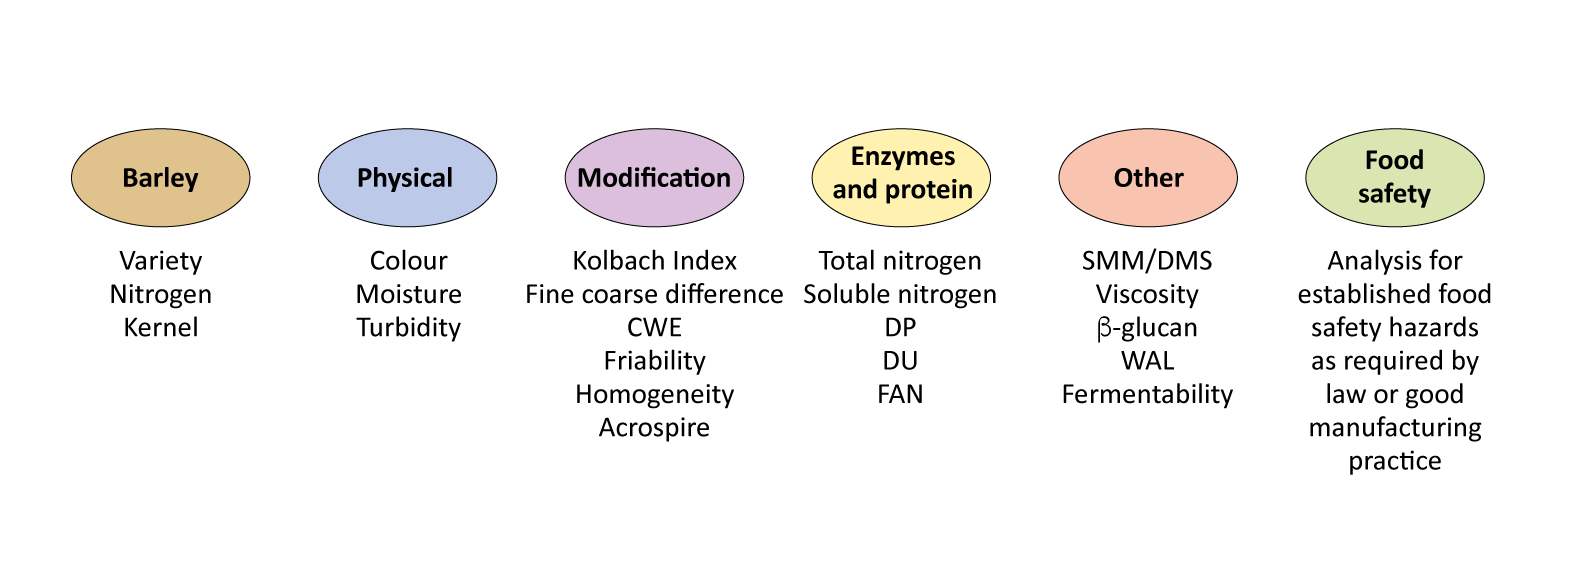
Figure: Malt quality parameters
Many of the analyses we cover in this lesson are not performed on the malt, but on wort produced from the malt. Below are the details of the laboratory mashes used to make this wort.
Key point: Standard mashes
IoB mash
Using a DLFU Buhler Miag disc mill, 50 g of malt is ground through a 0.7 mm screen to ensure the grain particles are less than 0.7 mm. This is added to 360 mL of; hot water in a flask to achieve a target temperature of 65°C. The flask is then maintained at 65°C for one hour and is stirred every 10 minutes. When the hour is complete, the mash is cooled to 20°C and the volume of the mash is topped up with water so it weighs 450 g. The mash is then filtered to recover the wort. This method can also be undertaken using malt ground through a 0.2 mm screen to provide a fine grind extract for the same malt. The difference in extract between the malt milled to 0.2 mm and the malt milled to 0.7 mm is called the fine coarse difference.The specific gravity of the wort is then measured by a pycnometer, densitometer, or hydrometer. This is used to calculate how much extract is available from the malt, which is expressed as Litre degrees per kilogram (L°/kg).
EBC (sometimes called Congress mash) and ASBC mash
These methods are similar to the IoB method but two temperatures are used. The same mill is used to produce 50 g of malt but this is ground with a 0.2 mm gap to ensure the grain particles are less than 0.2 mm. This is added to 200 mL of warm water in a flask to achieve a target temperature of 45°C. The flask is then maintained at 45°C for 30 minutes stirring constantly. After 30 minutes, the temperature is raised by 1°C per minute for 25 minutes. When 70°C is reached, a further 100 ml of water at 70°C is added and the mash is held at 70°C for 60 minutes. When the hour is complete, the mash is cooled to room temperature and the volume of the mash is topped up with water so it weighs 450 g. The mash is then filtered to recover the wort. The EBC method can also be undertaken using malt ground with a 1 mm mill gap to provide a coarse grind extract for the same malt. The difference in extract between this and the malt milled to 0.2 mm is called the fine coarse difference. The density of the wort is then measured by a pycnometer, densitometer, or hydrometer. This is used to calculate how much extract is available from the malt, which is expressed as percentage mass of extract.
The worts produced by standard mashes are also used to determine wort pH, colour, β-glucan, turbidity, FAN and fermentability.
Extract is reported in two ways. Extract can be quoted on an as-is basis, meaning that the moisture in the grain at the time of sampling has been included. Alternatively, we can describe it as dry or dwb (dry weight basis), meaning that although the test is done on the sample as-is, the percentage moisture is taken into account to calculate a value based on what would be present if the sample was absolutely dry. To calculate the dwb of a malt sample we can use this equation:

As an example, a malt with 5% moisture, and 76% as-is extract is 80% extract on a dry weight basis, as shown below:
