
Lesson 4 - Clarification – Centrifugation
This lesson discusses beer clarification via centrifugation. Clarification removes yeast and solid particles from the beer in order to make it ‘bright’ or reduce the amount of haze. Centrifugation is one method that we can use to clarify beer. This lesson looks closely at the physics of centrifugation and the concept of accelerated gravitational force. By the end of the lesson, you should understand the importance of this process and its impact on final beer quality.
Turbidity Control
We have mentioned the importance of beer turbidity control during centrifugation, but how do we achieve this?
Turbidity measurement is an optical analysis method. It detects the intensity of scattered light emitted by a light source. The intensity of scattered light is detected by photodetectors positioned at specific angles around the measuring cell, namely 90° and 25° scattered light:
-
Scattered light at 90° is used to detect the presence of small particles.
-
25° (forward scattering) is used to detect large particles.
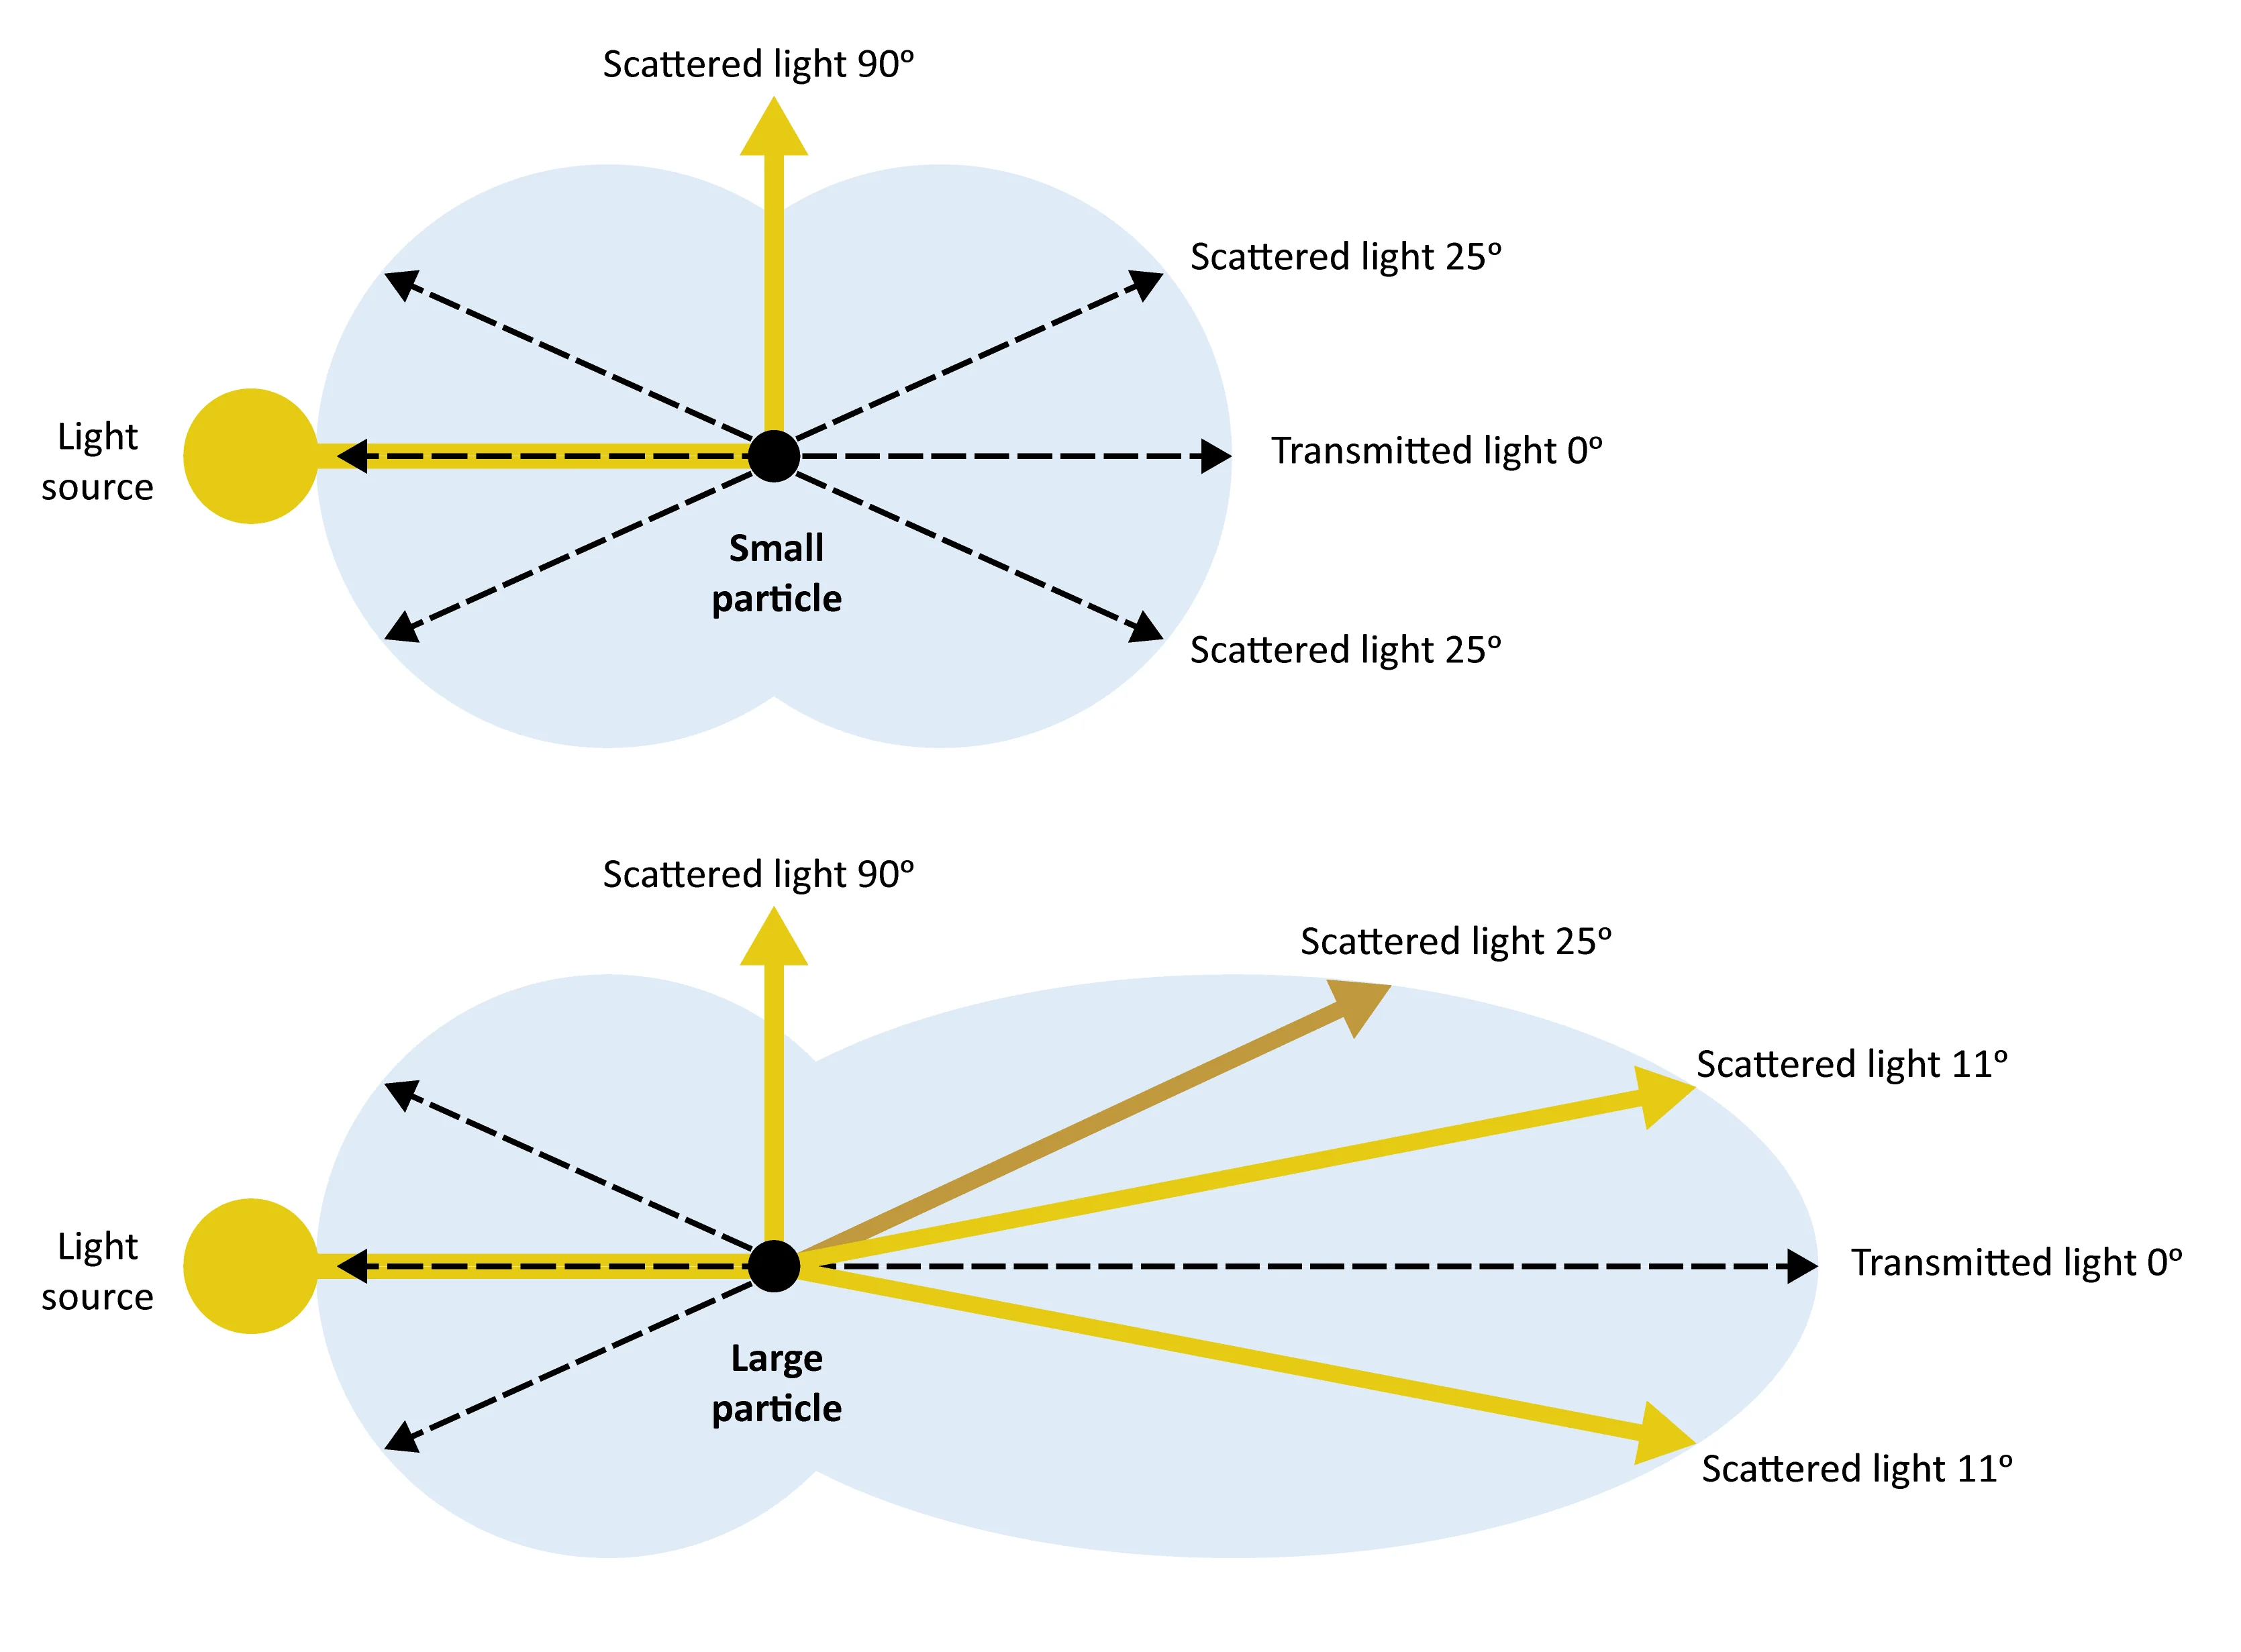
Figure: Scattered light intensity for detecting small and large particles
So, using a turbidity meter allows the brewer to determine the liquid’s transparency, which takes into consideration all sizes of particles, regardless of the sample’s colour.
The figure below shows where the in-line turbidity meter is positioned in the clarification process to allow the brewer to optimise the process to achieve the required clarity:
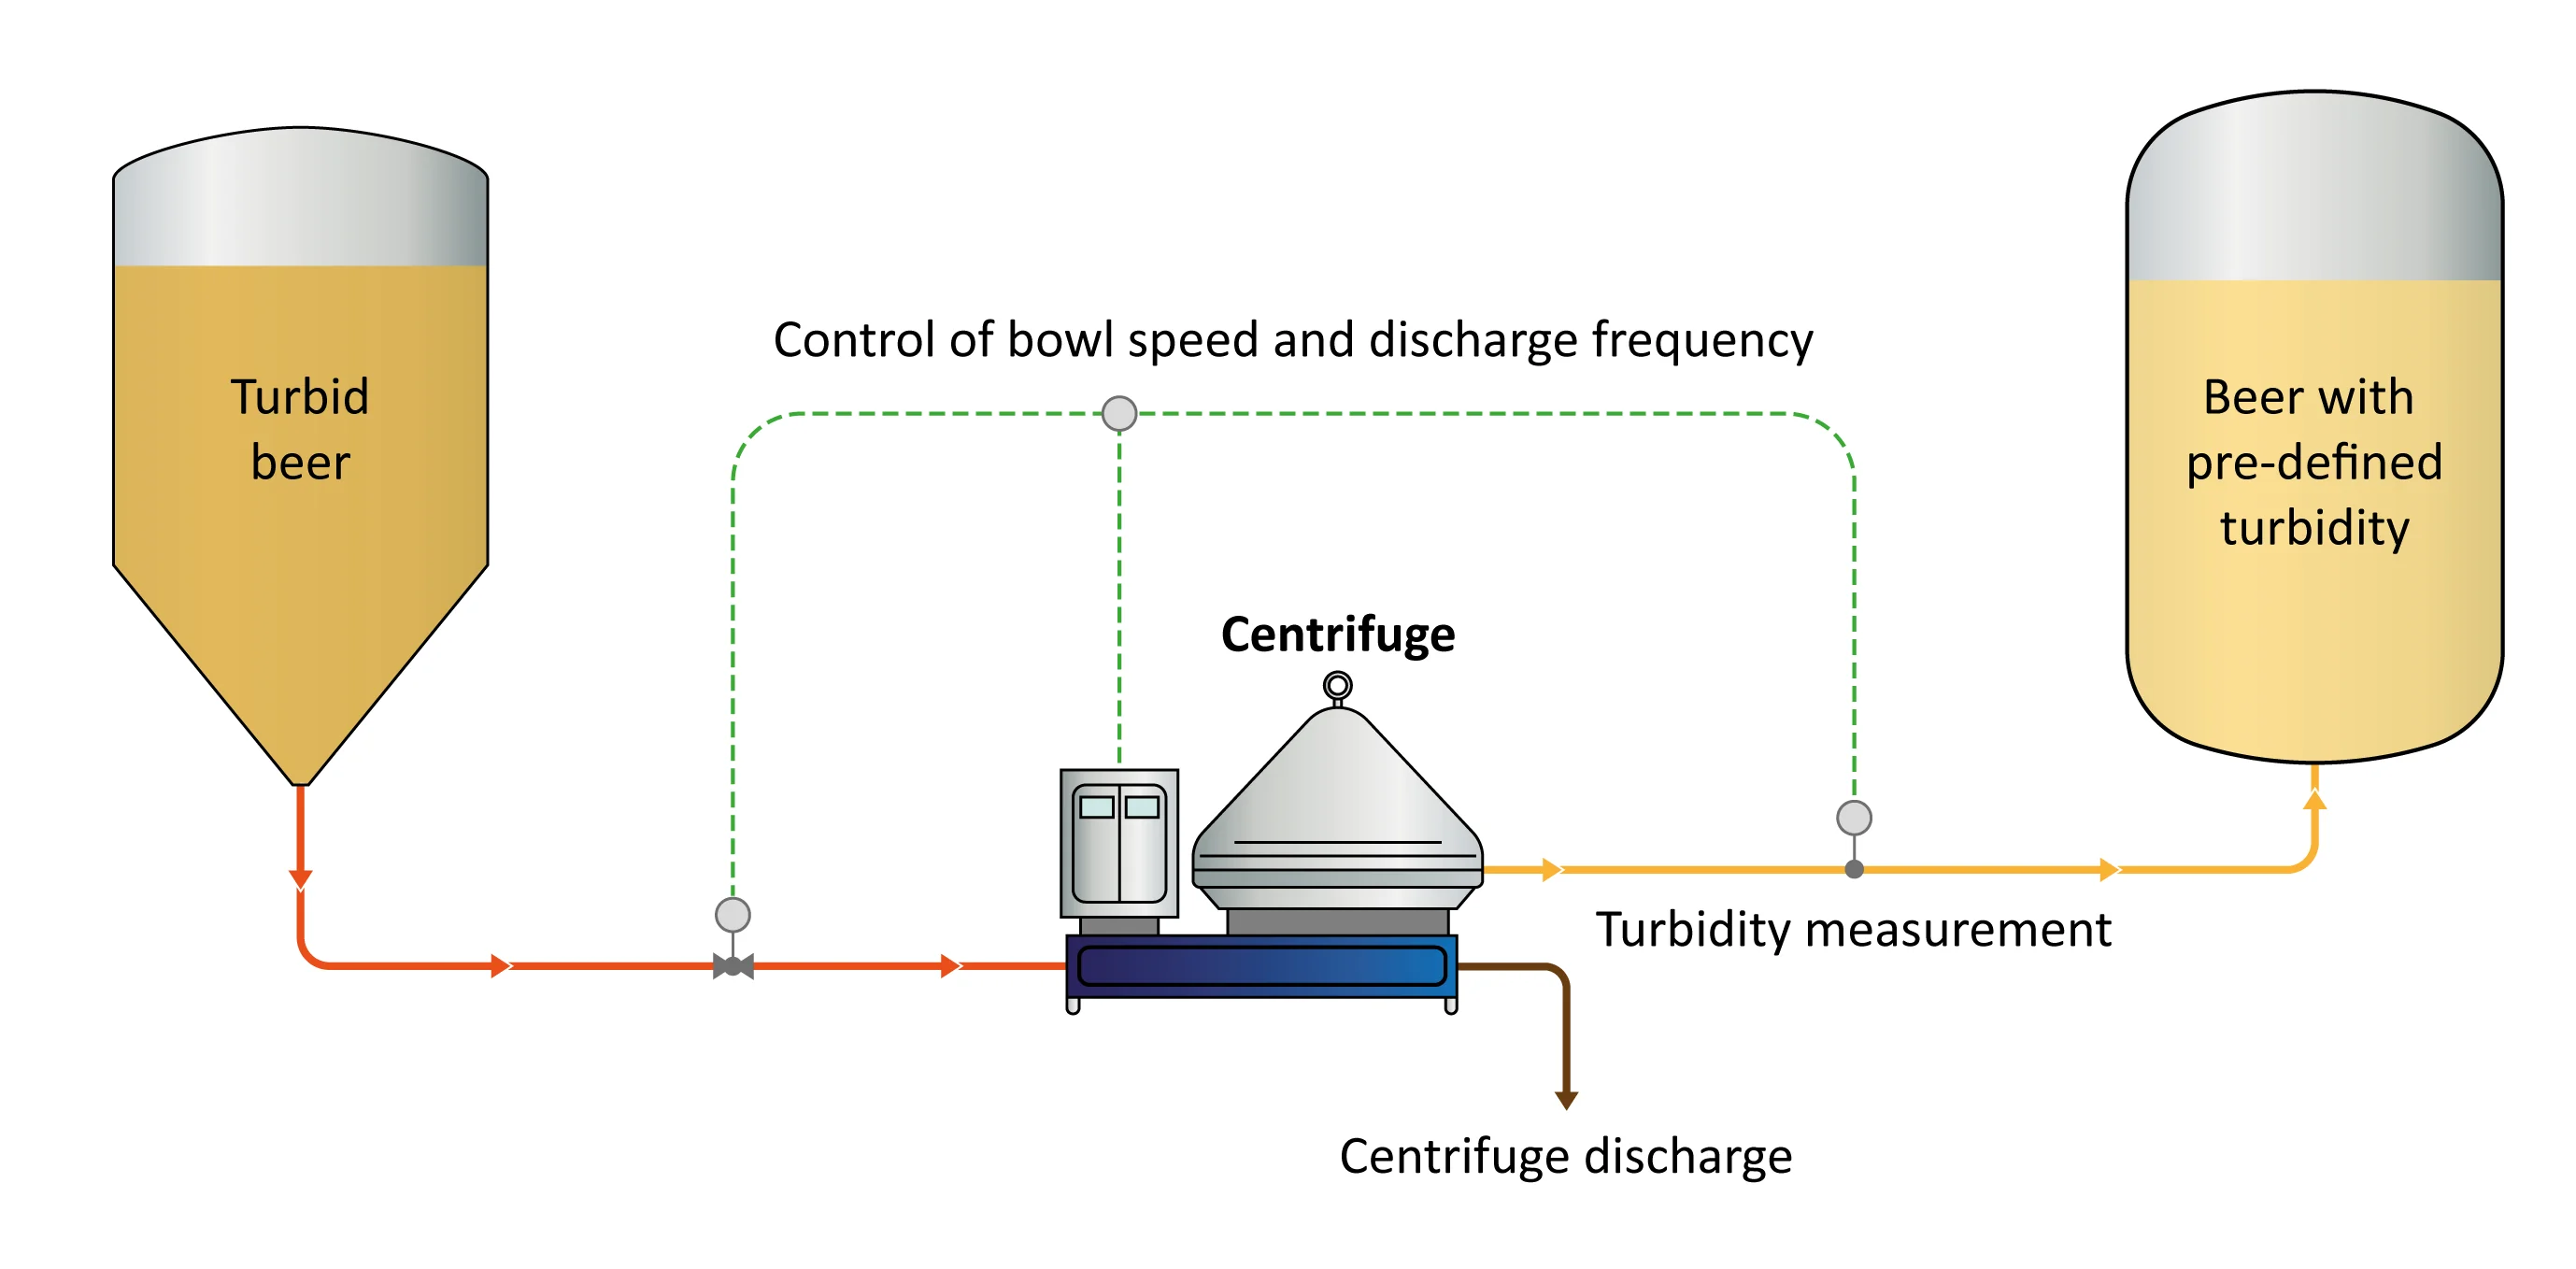
Figure: In-line turbidity meter set-up
The turbidity is constantly measured during transfer of the beer from the source vessel (e.g. the fermentation vessel) to the destination vessel (e.g. the maturation vessel). As the beer leaves the centrifuge (remember we used the term centrate), the turbidity is measured and the result is then fed back automatically to the centrifuge process control system. The centrifuge then automatically adjusts the centrifuge speed, solids discharge rate, and beer flow rate to achieve the beer clarity specification.
Commercial examples of in-line turbidity meters include:
Sigrist PhaseGuard T and TurbiGuard
Note, this is for illustrative purposes only and is not a recommendation or endorsement of a particular supplier’s product.